Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
WeChat17782577059
Engineered for rapid bioavailability and pristine sensorial aesthetics, our proprietary botanical powders support inner anti-aging, UV defense, dermal hydration, and cellular collagen renewal.
From topical serums to cellular replenishment: why functional drink mixes are outperforming traditional beauty delivery formats worldwide.
The intersection of dermatological science and dietary nutrition has birthed a multi-billion-dollar global nutricosmetics revolution. Modern beauty consumers no longer rely solely on topical serums, creams, and cosmetic procedures. Instead, the paradigm has decisively shifted toward "Beauty from Within" (Ingestible Beauty). Within this thriving segment, Solid Beverage Powder OEM has emerged as the premier manufacturing format, driven by consumer demand for high-potency bioactives, instantaneous solubility, shelf stability without synthetic preservatives, and an engaging lifestyle hydration ritual.
Compared to ready-to-drink (RTD) liquid beverages, softgels, or standard hard tablets, solid beverage powders represent an engineering pinnacle for cosmetic compounding:
Proprietary fluid-bed granulation binds active extracts into porous micro-granules, preventing static clumping and achieving zero-residue instant cold-water dispersion within 8 seconds.
Advanced sensory masking technology neutralizes fishy peptide notes, metallic mineral aftertastes, and bitter botanical astringencies using real freeze-dried fruit powders and organic acid matrices.
Low-heat vacuum evaporation and sub-zero freeze crystallization preserve 98.4% of native Vitamin C, Salvianolic Acid B, enzymatic polyphenols, and fragile anthocyanin chromophores.
Modern nutricosmetic contract manufacturing requires multi-targeted botanical compounding. We formulate solid beverage powders designed to tackle skin health through four biological pathways.
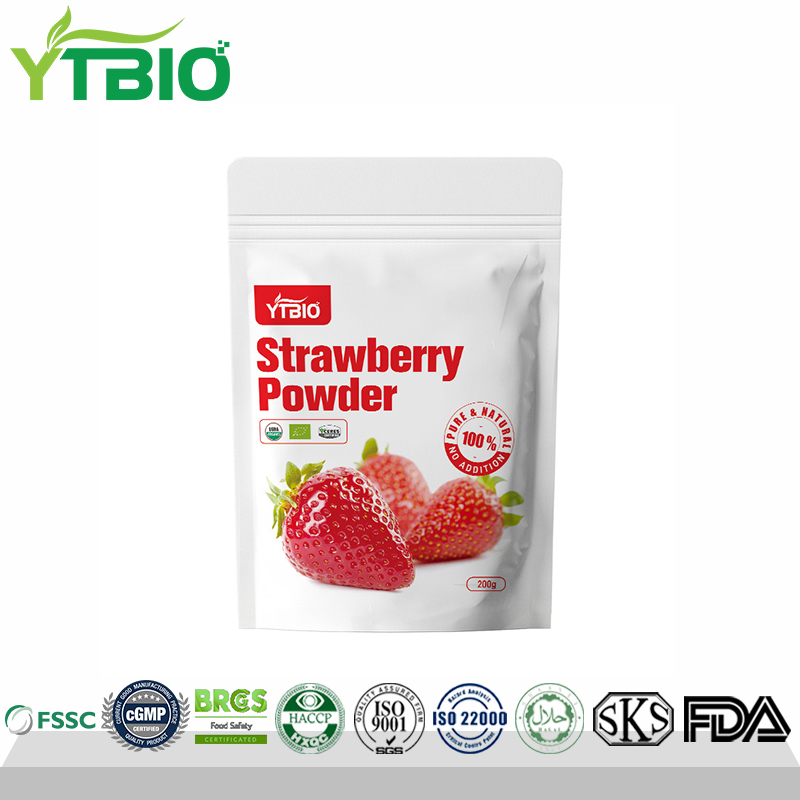
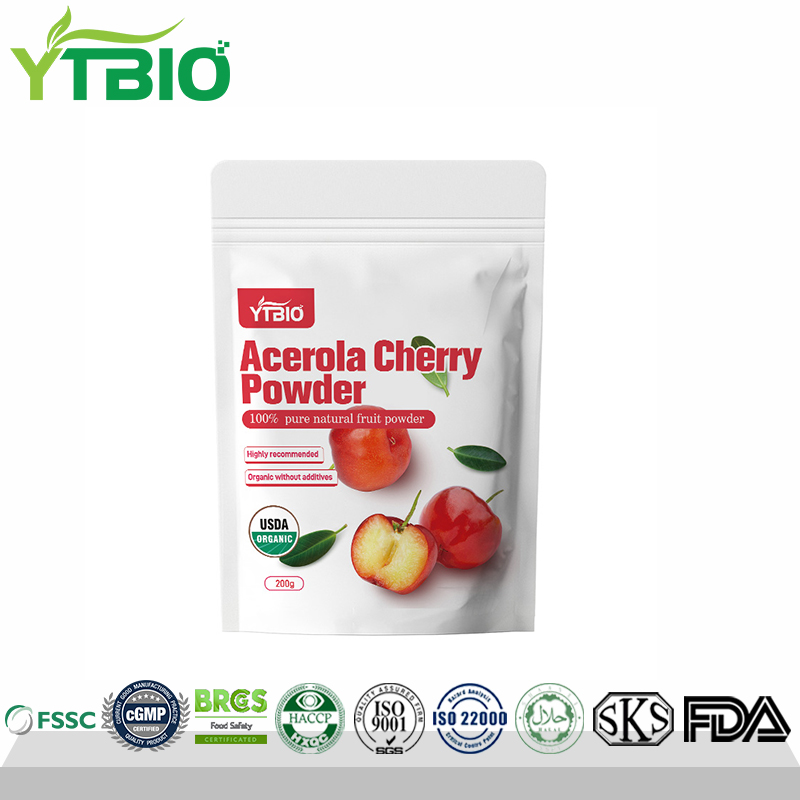
Skin aging is structurally characterized by the progressive fragmentation of the extracellular dermal matrix (ECM) and diminished Type I and Type III collagen synthesis by dermal fibroblasts. Our OEM solid beverage solutions integrate low-molecular-weight marine collagen oligopeptides (<1000 Da) coupled with natural ascorbic acid cofactors sourced from Organic Acerola Cherry Extract Powder.
Ascorbic acid acts as an essential cofactor for prolyl and lysyl hydroxylases, stabilizing the collagen triple-helix architecture. Coupled with silicon-rich bamboo extracts and amino acid building blocks, this solid drink format triggers endogenous procollagen gene expression while attenuating Matrix Metalloproteinase (MMP-1) collagen degradation.
Hyperpigmentation, solar lentigines, and post-inflammatory erythema stem from overactive tyrosinase enzymatic cascades in melanocytes. By compounding high-potency Mulberry Extract Powder (rich in Mulberroside A, oxyresveratrol, and anthocyanins) with active Salvianolic Acid B, our solid drink powders deliver potent free-radical quenching against ultraviolet UVA/UVB-induced reactive oxygen species (ROS).
This dual active synergy inhibits tyrosinase monophenolase and diphenolase activities, accelerating epidermal cell turnover to purge accumulated melanin, leaving a visibly brighter, even-toned complexion.


Transepidermal water loss (TEWL) is the primary precursor to micro-wrinkles, xerosis, and irritated skin barrier function. Solid beverage formulation enables the stabilization of high-viscosity hydrophilic polymers like Food-Grade Sodium Hyaluronate (HA) alongside natural fruit electrolyte bases such as Premium Watermelon Fruit Powder and Pure Freeze-Dried Papaya Powder.
Watermelon powder delivers high concentrations of L-citrulline and natural potassium ions, facilitating cellular osmoregulation and microvascular perfusion, while enzymatically active papaya bioactives support intestinal nutrient absorption, hydrating the cutaneous layer from within.
Advanced Glycation End-products (AGEs) crosslink with dermal structural proteins, leading to skin stiffness, dull sallow pigmentation, and loss of rebound elasticity. By formulating powdered beverage bases with polyphenol-dense Matcha Powder and synergistic digestive enzymatics, our formulas assist in blood glucose stabilization, intercepting glycation before sugar molecules can chemically bond to dermal elastic fibers.
Your premier manufacturing partner with 10+ years of deep expertise in raw material cultivation, botanical extraction, and advanced contract OEM/ODM compounding.
Shaanxi Yuantai Biological Technology Co., Ltd. was established in 2014. Its headquarter is located in Xi'an and its factory is located in Weinan Economic and Technological Development Zone. The factory covers an area of 10000+㎡.
At present, the company's main categories include: capsules, granules, tablets, solid beverages, soft candies and other OEM categories. YTBIO has 10 years of production experience in the raw material field. The main categories include: herbal extracts, nutritional supplements, organic extract raw materials and cosmetic raw materials.
YTBIO is a comprehensive health food manufacturer. With its understanding of the raw material industry and products, it uses industry experience to provide compounding solutions from raw materials to finished products, and supports professional solutions in product packaging, flexible application of ingredients, and product label design. In addition, we are also committed to developing new products to provide customers with more product and formula options to meet the various needs of different customers for products.


YTBIO's production facilities and equipment meet national standards, and the production process is strictly carried out in accordance with GMP requirements. The raw materials meet national standards, and after comprehensive inspection and quality control, the production process is strictly carried out in accordance with scientific production process to ensure the safety, stability and effectiveness of the products. In order to provide customers with satisfactory products and services, we have established a modern quality management system in accordance with international standards, including inspection and testing of raw materials, intermediates, and finished products, as well as full monitoring of the production process to ensure that product quality meets standards.

The factory has standardized R&D rooms and inspection rooms, and a 100,000-level GMP purification workshop. Using professional production experience, leading equipment, and professional technology, production is carried out in accordance with standardized processes. Strict standards have been set for every link in the production process. The raw materials are all from well-known manufacturers at home and abroad. Each batch of products produced is checked and inspected before leaving the factory. Excellent inspection capabilities ensure that the quality is strictly controlled from raw materials to semi-finished products to finished products. We insist on in-depth development and utilization of new food resources to contribute wisdom and strength to human health!

In the 10 years of development, the company has continuously improved its corporate management level, strengthened quality management, managed in accordance with the requirements of the international standardized quality management system, and passed a number of certifications. We will further optimize and standardize various management systems, continuously improve the effectiveness of the system operation, continuously improve the company's management level, and jointly promote the rapid development of the company.
To ensure product quality and production process standards, we have passed cGMP, FSSC22000, BRC, HACCP, ISO9001, ISO22000, HALAL, KOSHER, FDA, and EU & US organic certifications.


OEM categories: capsules, granules, tablets, solid beverages, etc. | OEM content: raw materials, formula, packaging, label design, etc.
Within our solid beverage production facilities we are able to offer the production of instant teas, granular beverages and pack them directly into finished products or in separate operations, for example:

Regarding capsules, we are able to provide finished packaging or production of separate operations, such as:

Complete custom manufacturing and packaging configurations for chewable, effervescent, and swallowable beauty tablets:
Use the highest quality plant raw materials from reliable suppliers, produce and process in our own factory, providing one-stop service. Extract and process with high technical standards to retain the highest quality ingredients of raw materials. Produce products such as capsules, tablets and solid drinks.
High-purity food-grade active raw materials, spray-dried fruit bases, and antioxidant bioactives ready for solid drink contract compounding.