Leave Your Message
Explore high-demand dietary supplements, botanical extracts, and pharmaceutical-grade encapsulated products ready for custom private labeling.
Modern pharmaceutical and healthcare sectors demand rapid commercialization, stringent biopharmaceutical stability, and innovative clean-label encapsulation technologies.
Surging consumer transition from traditional bovine/porcine gelatin towards Non-GMO, vegan-certified HPMC and pullulan plant polymers.
Engineering gastro-resistant (HPMC-DR) and enteric profiles protecting acid-sensitive probiotics, enzymes, and active pharmaceutical ingredients (APIs).
Integration of high-speed filling lines, micro-dosing systems, and digital batch tracking to guarantee ±1% filling weight homogeneity.
End-to-end dossier assistance for global markets, spanning FDA registration, EU organic standards, Kosher, Halal, and ISO conformity.
The global pharmaceutical and nutraceutical capsule manufacturing sector is experiencing unprecedented growth, projected to expand at a robust compound annual growth rate (CAGR). This expansion is largely propelled by aging demographics, heightened focus on preventive well-being, sports nutrition, and the clinical validation of functional botanicals.
Contract Development and Manufacturing Organizations (CDMOs) and OEM/ODM specialists are no longer just toll-manufacturers. Today's commercial environment expects contract manufacturers to be end-to-end formulation innovators. From identifying potent synergistic raw materials to tailoring dissolvability kinetics in gastrointestinal microenvironments, modern capsule OEM requires an intersection of phytochemistry, material sciences, and automated engineering.


Shaanxi Yuantai Biological Technology Co., Ltd. (YTBIO) was established in 2014. Its headquarters is located in Xi'an and its modern manufacturing factory is located in the Weinan Economic and Technological Development Zone. The factory covers an expansive area of 10,000+㎡ (with an initial core facility footprint of 6,700 ㎡).
At present, the company's main categories include: capsules, granules, tablets, solid beverages, soft candies (gummies), and other comprehensive OEM / ODM categories.
YTBIO possesses over 10 years of specialized production experience in the raw material field. Our primary categories include herbal extracts, nutritional supplements, organic extract raw materials, and cosmetic raw materials. As a comprehensive health food manufacturer with a profound understanding of raw material properties, we leverage industrial experience to provide compounding solutions from active raw ingredients to finished shelf-ready products, complete with tailored packaging and professional label design.
Operating Class 100,000 cleanrooms and advanced quality management protocols compliant with global pharmaceutical norms.

YTBIO's production facilities and equipment meet stringent national standards, and the production process is strictly carried out in accordance with GMP requirements. The raw materials meet national standards, and after comprehensive inspection and quality control, the production process is executed through scientific protocols to ensure the safety, stability, and effectiveness of every batch.

The factory has standardized R&D rooms, modern analytical inspection labs, and a 100,000-level GMP purification workshop. Utilizing cutting-edge encapsulation lines, raw materials from well-known global suppliers undergo rigorous QA/QC. Each batch is inspected prior to release, safeguarding quality from raw botanicals to finished dosages.

In over 10 years of rapid development, the company has continuously perfected corporate governance, strengthened testing capabilities, and operated strictly in compliance with international standardized quality management systems. We continuously optimize our standard operating procedures to deliver exceptional contract manufacturing reliability.

We provide a comprehensive range of capsule shell polymers and dimensional sizes customized for both pharmaceutical and dietary supplement dosage requirements:
Supported standard sizes: #000, #00, #0, #1, #2, #3, #4, with customized shell coloring, transparent clarity, titanium-dioxide-free opaque finishes, and pearlized branding.
Weighing & homogenizing of active raw ingredients, micro-powder blending, high-precision encapsulation of prepared mixtures, metal detection, visual sorting, and multi-format packaging.
Full-spectrum formulation and packaging customizability across solid dosage formats.
Our automated high-speed tablet presses offer flexible hardness, rapid disintegration, chewable profiles, and effervescent options tailored for clinical and consumer applications.
Tablet Packaging Specifications: 10 tablets, 15 tablets, 30 tablets per blister or bottle; aluminum-plastic blister packs, child-resistant bottles, and sales box outer packaging.

Within our solid beverage production facilities, we produce instant teas, functional electrolyte blends, meal replacement shakes, and granular dietary beverages packed directly into versatile retail packaging:

We utilize the highest quality plant raw materials from reliable global and domestic suppliers, producing and processing directly in our own facilities for true one-stop efficiency.
Extracting active phyto-compounds with high technical standards to retain the highest biological activity. Utilizing super-critical CO2, solvent extraction, membrane concentration, and spray-drying towers.
Every inbound botanical, amino acid, and mineral undergoes strict identity verification via HPLC, GC-MS, TLC, along with heavy metal testing (ICP-MS) and pesticide residue screening.
Synergizing active herbal extracts directly with excipients to create stabilized capsules, tablets, and drinkable powders without unnecessary synthetic additives.
Custom encapsulation solutions engineered for clinical efficacy, targeted absorption, and brand differentiation.
Formulations utilizing Tetrahydrocurcumin, CoQ10, and botanical flavonoids designed for arterial integrity, healthy lipid metabolism, and glucose modulation.
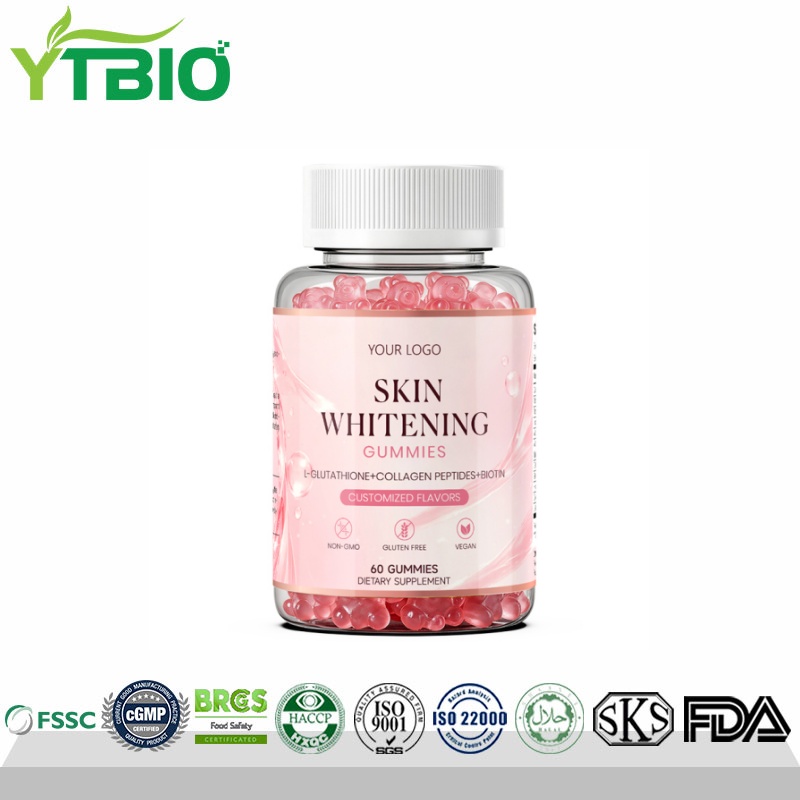
Skin rejuvenation capsules combining reduced L-Glutathione, Hyaluronic Acid, Collagen peptides, and Vitamin C for cellular photoprotection and dermal hydration.
Instantized 2:1:1 BCAAs, Calcium D-Gluconate, electrolytes, and anti-inflammatory extracts for rapid muscle recovery, joint lubrication, and peak physical endurance.
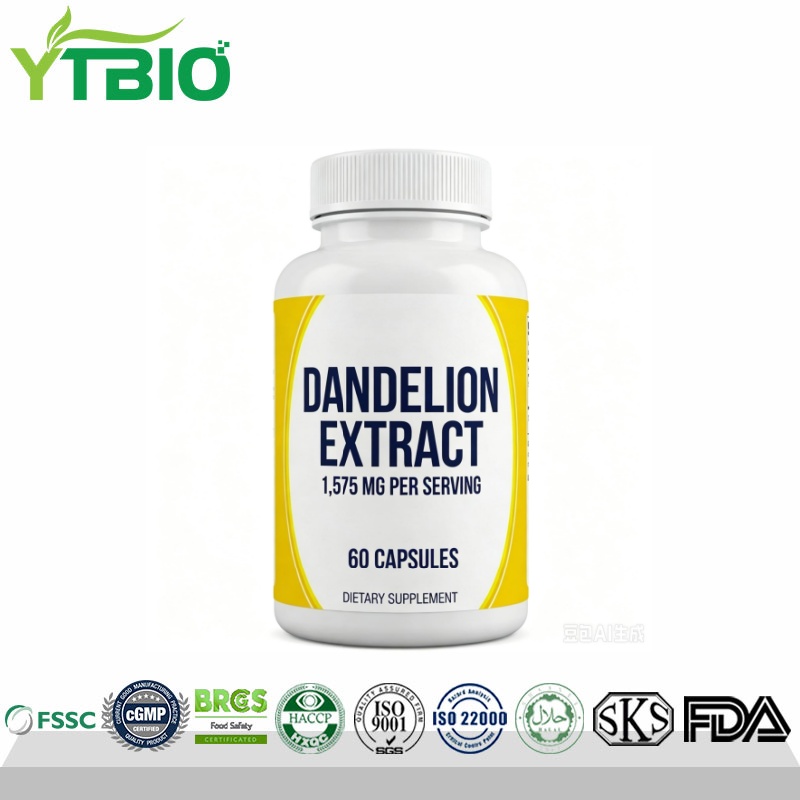
Targeted delayed-release capsules delivering Dandelion Extract, Milk Thistle, Apple Cider Vinegar, and probiotic flora directly to the lower digestive tract.
To ensure product quality and standardized manufacturing processes, we have acquired comprehensive global credentials: cGMP, FSSC22000, BRC, HACCP, ISO9001, ISO22000, HALAL, KOSHER, FDA, EU & US Organic Certifications.


From bulk manufacturing to bespoke retail shelf packaging, our automated lines accommodate diverse presentation needs.
High-barrier Alu-PVC and Alu-Alu blister configurations (10, 15, 30 count plates) providing superior humidity isolation and convenient portable dosing, inserted into custom display sales boxes.
HDPE, PET, and amber glass bottles (30 to 240 count) with induction sealing, child-resistant or screw caps, tamper-evident shrink bands, and waterproof embossed labeling.
Dedicated in-house design engineers delivering multi-lingual regulatory compliance checks, barcode registration, aesthetic finish treatments, and market-ready box packaging.
Discover our comprehensive range of private label capsules, functional powders, and specialized botanical extracts.